

With years of experience selling and servicing fiber laser cutting equipment, Fab-Line’s team sees the same nozzle mistakes on the shop floor again and again. The nozzle costs twenty to forty dollars. A bad one costs you a scrapped part, a damaged lens and an unplanned stop on a job you already quoted. If your fiber laser is leaving dross, cutting slower than it should, or giving you inconsistent edges on the same program that worked fine last month, the nozzle is one of the first places to look, right behind the lens and the focus position.
What does a fiber laser cutting nozzle actually do?
The nozzle is the small threaded part at the tip of the cutting head that directs the assist gas (oxygen, nitrogen or compressed air) into the kerf alongside the laser beam. It shapes the gas stream, controls how much gas reaches the cut, and sets how close the beam can get to the material before gas pressure drops off. A worn or mismatched nozzle changes the gas flow pattern even when every other setting on the machine is correct, which is why operators chase a “machine problem” for hours when the fix is a five dollar part.
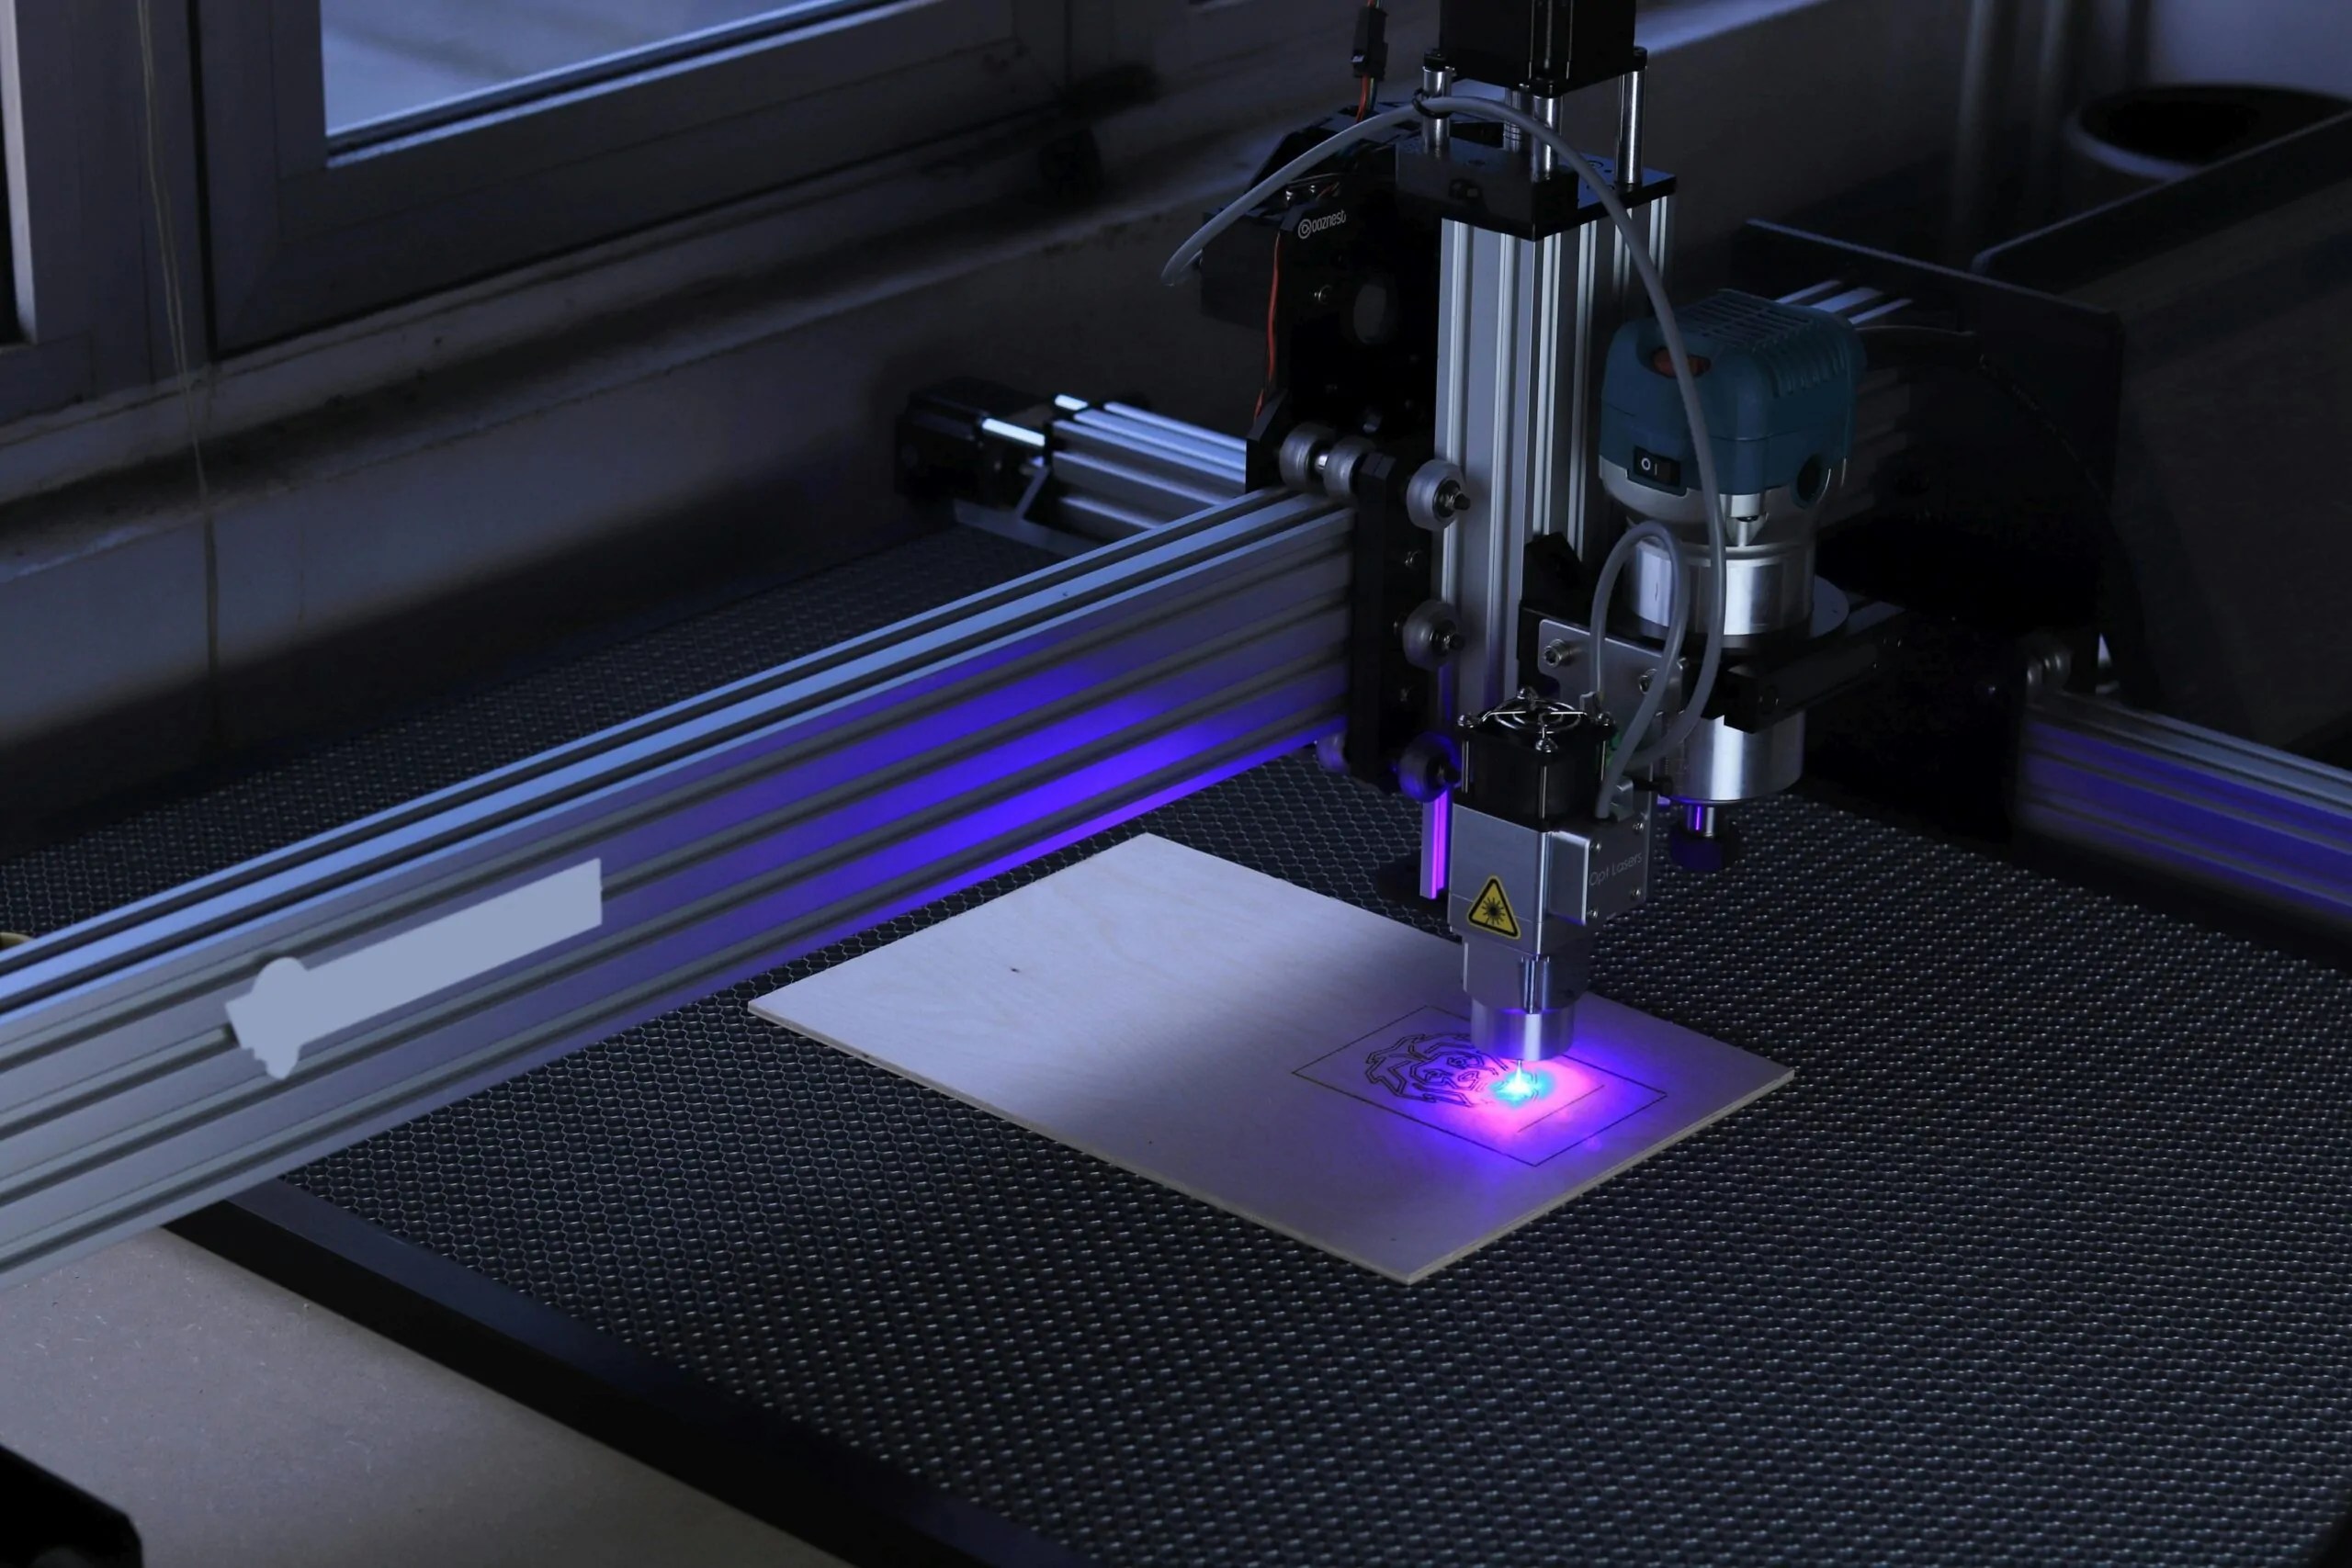
Single-layer vs double-layer nozzles: which do you need?
Single-layer nozzles pass gas through one channel and work well on thin material, light power and jobs where edge quality is secondary to speed. Double-layer nozzles separate the gas flow into an inner and outer stream, which stabilizes pressure at higher power and on thicker material, and is the standard choice for most job shops running 3kW and up on carbon steel or stainless over roughly 6mm.
| Nozzle type | Best for | Trade-off |
|---|---|---|
| Single-layer | Thin sheet (under ~3mm), lower power machines, fast turnaround jobs | Less stable gas flow at high power or on thick material |
| Double-layer | Mid to thick material, 3kW+ machines, stainless and aluminum where edge quality matters | Higher consumable cost, needs more frequent inspection |
How do I choose the right nozzle diameter?
Diameter is matched to material thickness and assist gas, not to the machine’s maximum power. A nozzle that is too small for the job starves the cut of gas and leaves dross on the bottom edge. One that is too large wastes gas, drops cutting speed and can let the beam wander off center inside the gas stream. As a rough shop-floor reference:
| Material thickness | Typical nozzle diameter | Typical assist gas |
|---|---|---|
| Up to 3mm mild steel | 1.0 to 1.5mm | Oxygen or nitrogen |
| 3mm to 10mm mild steel | 1.5 to 2.0mm | Oxygen (economy) or nitrogen (clean edge) |
| Stainless steel, most gauges | 1.5 to 3.0mm | Nitrogen (oxide-free edge) |
| Aluminum | 2.0 to 3.5mm | Nitrogen, higher pressure |
These are starting points, not a substitute for your machine builder’s own chart. Every control system ties nozzle diameter to a specific pressure and focus setting in its cutting parameter library, and the fastest way to go wrong is to swap a nozzle without updating the program that calls for it.
What is standoff distance and why does it matter?
Standoff distance is the gap between the nozzle tip and the top of the material, usually set between 0.5mm and 1.5mm depending on thickness and gas type. Too close and the nozzle risks contact with a warped sheet or spatter buildup, which can damage the protective lens behind it. Too far and the gas stream loses pressure before it reaches the kerf, which shows up as rough, angled cut edges and increased dross, especially on thicker material where the beam needs a tightly focused gas column to push molten metal through the full depth of the cut.
How do I know when a nozzle is worn out?
A nozzle wears from spatter, heat and the physical orifice widening slightly every time the machine strikes an arc through it. Watch for these three signs rather than running nozzles until they visibly fail:
- Dross returning on a program that used to cut clean. If nothing else changed, check the nozzle orifice for widening or an off-center opening before you touch the gas pressure.
- Cut speed drops without a program change. A damaged or spattered nozzle disrupts gas flow and forces the controller (or the operator) to compensate with slower feed rates.
- Visible pitting, scoring or an elongated (no longer round) orifice. Any of these means the gas stream is no longer symmetrical around the beam, which shows up as an inconsistent edge on one side of the cut versus the other.
Most shops replace nozzles on a cycle count or run-hours basis rather than waiting for a visible failure, since a nozzle that is 80 percent worn still looks fine to the eye but is already costing cut quality.
Does nozzle choice change with assist gas?
Yes, and this is where shops lose the most time. A nozzle sized correctly for nitrogen at high pressure will not perform the same way on oxygen at low pressure, because the two gases are doing different jobs. Oxygen reacts exothermically with the material to help burn through it, so the nozzle only needs to deliver a steady, lower pressure stream. Nitrogen is inert and relies entirely on sheer gas force to blow the molten metal out of the kerf, so it typically needs a larger orifice and far higher pressure, often 15 to 20 bar versus 1 to 3 bar for oxygen cutting. Running the wrong nozzle for your gas choice is a common reason a shop’s nitrogen cuts look worse than its oxygen cuts even though the machine and material are identical.
Frequently asked questions
How often should fiber laser nozzles be replaced?
Replacement intervals depend on material, thickness and duty cycle, but most job shops inspect nozzles daily on high-volume machines and replace them on a fixed cycle count rather than waiting for visible damage, since cut quality degrades before the wear is obvious to the eye.
Can the wrong nozzle damage my machine?
A nozzle that is damaged, loose or contacts the material can let spatter reach the protective lens or the cutting head itself, which is a far more expensive repair than the nozzle. Checking nozzle condition and seating is part of routine daily maintenance for this reason.
Do all fiber laser brands use the same nozzle sizes?
No. Nozzle threading and sizing are specific to the cutting head manufacturer, so a nozzle for one machine will not fit another even when the stated diameter is the same. Always order from your machine’s parts list rather than a generic size match.
What is the single biggest nozzle mistake shops make?
Running a worn or mismatched nozzle because it still “looks fine,” rather than tracking cycle counts or inspecting under light. Nozzle wear is one of the few cutting problems with a cheap, fast fix once it is actually diagnosed as the cause.
If you are evaluating a new fiber laser cutting machine and want to understand the real cost of ownership, including consumables like nozzles, lenses and gas, our team can walk through the numbers for your part mix and material thickness. Contact Fab-Line or ask about our service and maintenance support for machines already on your floor.
Questions about nozzle wear, consumable costs or maintenance on a machine you already own? Call Fab-Line at (888) 317-3615 or reach out here.
Further reading on assist gas and nozzle technology: Precitec’s laser cutting head and nozzle technology overview.